Để có phản hồi nhanh hơn, xin vui lòng bao gồm số WhatsApp hoặc Skype của bạn trong tin nhắn của bạn để chúng tôi có thể liên lạc với bạn càng sớm càng tốt.
Để giúp chúng tôi phản hồi nhanh hơn, xin vui lòng để lại WhatsApp, email hoặc chi tiết dự án của bạn. Chúng tôi thường phản hồi trong vòng 24 giờ. Đối với các yêu cầu khẩn cấp, liên hệ với chúng tôi qua WhatsApp: +8617862411260 hoặc WeChat: +8617862411260. gọi cho chúng tôi trực tiếp.
lucy| Founder, Senserui | Published: 20 August 2026 · Last reviewed: 20 August 2026 Technical review: Senserui Engineering Team
An industrial woodworking dust collection system for a production plant means centralized extraction in the 30,000–150,000 m³/h range, ducted to every machine, with a dust silo for storage and explosion protection built in. Shop collectors rated in horsepower solve a different problem at roughly one-tenth the airflow.
Look up woodworking dust collection and the results split cleanly in half. One half is application overviews from equipment brands, describing why wood dust is a problem without publishing a single airflow figure or dimension. The other half is machinery retail: cyclone units rated 5 to 20 horsepower, priced, in stock, shipping next week.
Neither addresses a furniture factory. The retail tier tops out at roughly 15 kW, which is where the industrial tier’s smallest compact units begin. A plant running twelve to thirty machining and sanding stations is looking at an order of magnitude more air than a 20 HP unit moves, plus a duct network, plus somewhere for several cubic metres of waste per shift to go.
Here is the actual equipment ladder, with published figures rather than category names:
| Tier | Rated power | Airflow | Published dimensions | What it serves |
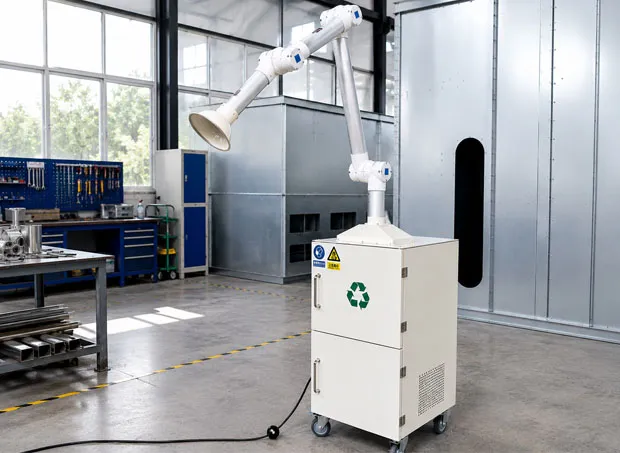
| Single-station | Giải đua W Series, 1.1–3 kW | 700–2,000 m³/h | approx. 700 × 350 × 1,360 mm | One welding, grinding or finishing point |
| Workstation table | PW Series grinding dust collection table | Not publicly disclosed | Compact; units can be arranged side-by-side | Individual sanding/finishing benches, replaceable filter elements, integrated fire-arresting structure |
| Small workshop | S Series, 3–15 kW | 3,000–15,000 m³/h | approx. 2,000 × 1,200 × 3,200 mm to 2,100 × 2,100 × 6,000 mm | A small shop or a fine-dust cell inside a larger plant |
| Factory centralized | CP / CC Series, 30–150 kW | 30.000–150.000 m³/h | L approx. 3,500–13,000 mm × W approx. 2,400 mm | A ducted plant-wide network |
The gap between 15,000 and 30,000 m³/h is where most furniture manufacturers actually sit when they first calculate their total, and it is exactly the gap the ranking pages skip.
A furniture plant is not producing “wood dust.” It is producing at least two materials with opposite handling requirements.
Coarse chips come off saws, planers, moulders and CNC routers. High mass, high volume, and they need transport velocity to stay suspended in the duct. They fill a silo fast.
Fine sanding dust comes off wide-belt sanders, edge sanders and orbital work, and MDF sanding is the extreme case. Low mass, high surface area, and it goes straight into the filtration media. It is also the fraction that stays airborne in the workshop and reaches operators’ breathing zones.
Senserui’s catalogue splits along that line rather than pretending one machine covers both:
So where does a plant with both draw the line? Three workable answers, in descending order of capital cost:
Option 2 is the one most often chosen and most often chosen for the wrong reason, which is that the quotation is smaller. Ask what the filter media replacement interval becomes under mixed loading before signing.
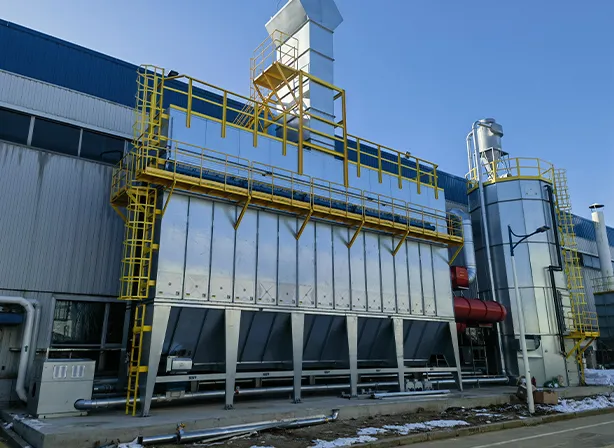
| Parameter | Published figure |
| Models | CP30 / CP60 / CP90 / CP120 / CP150 |
| Rated power | 30–150 kW |
| Airflow | 30.000–150.000 m³/h |
| Equipment length | approx. 3,500–13,000 mm |
| Width | approx. 2,400 mm |
| Overall height | approx. 7,000 mm |
| Operating noise | <80 dB |
| Particulate emission target | <5 mg/m³ |
| Designed for | Fine and ultrafine dust: sanding, fine grinding, polishing, CNC processing |
Two of those rows do more work than the rest.
The 7,000 mm height determines whether the unit goes inside the building or onto an external pad. Existing furniture workshops frequently have an eave line below that, and the CC Series alternative is taller still at approximately 8,500 mm. Measure the clear height under the lowest obstruction — roof truss, crane rail, sprinkler main — before the layout is drawn. Discovering the clash at delivery costs a foundation.
The <80 dB figure matters because the mainframe usually ends up near the building wall, and in a plant where operators work a full shift within a few metres of it, that number belongs in the specification alongside the airflow.
The 30,000–150,000 m³/h span is covered in five model steps. A plant whose calculated total lands between steps should have the specific model figures confirmed rather than interpolating from the range endpoints. If the total is under 30,000 m³/h, the S Series covers 3,000–15,000 m³/h for fine-dust duty.
Price is available on request based on system configuration and project requirements. Airflow, dust characteristics, plant layout, ducting, filtration configuration, safety requirements and automation level all move the figure, which is why no per-model list price is published.
Small shops empty a drum. A furniture factory generates waste faster than anyone wants to handle manually, and the collection interval, not the collector, is what dictates silo size.
Dòng MS integrated dust bin system — MS30 through MS150:
That 3,100 mm discharge height is the number to check first, because it has to clear whatever collects the material underneath. A standard high-cube container or a tipper bed either fits under it or does not, and no amount of system tuning fixes the answer afterwards. Confirm the vehicle before confirming the silo.
Where yard space is already committed, the Dòng DC modular tower silo trades footprint for height: 5–15 kW, 30–100 m³ storage, diameter 2,400–4,500 mm, height 10,000–18,000 mm. The product page states the system is designed with reference to relevant national and EU standards; a specific product certificate number is not published. Tower silos also introduce a foundation and a crane lift into the installation programme, which pushes the schedule.
Sizing method: kilograms of waste per hour × hours between collections ÷ bulk density. Wood waste bulk density varies enormously between planer shavings and sanding dust, so run the calculation on the mix your plant actually produces rather than on a handbook value for one of them.
Wood dust is a combustible particulate solid, and the storage silo concentrates it.
NFPA 660 — Standard for Combustible Dusts and Particulate Solids, 2025 Edition, published by the National Fire Protection Association, is the consolidated standard covering fire and explosion hazards for this material class. It addresses dust hazard analysis, explosion protection, housekeeping and equipment provisions in one document. The dust hazard analysis belongs at the front of the project, because its findings determine hardware that cannot be retrofitted cheaply.
In the United States, OSHA publishes standards and guidance on combustible-dust hazards under general-industry regulations. For equipment operating in or sold into the EU, the ATEX framework (Directive 2014/34/EU, European Commission) governs equipment and protective systems intended for use in potentially explosive atmospheres.
On the Senserui side, the accurate wording is that explosion protection is designed based on ATEX principles. Product-specific certificate numbers, issuing bodies and notified-body references are not published. That distinction is worth holding onto during procurement: “designed based on ATEX principles” and “ATEX certified” are different claims, and if your project requires the latter, request the document rather than accepting the phrase. This applies to every supplier you evaluate, not only to this one.
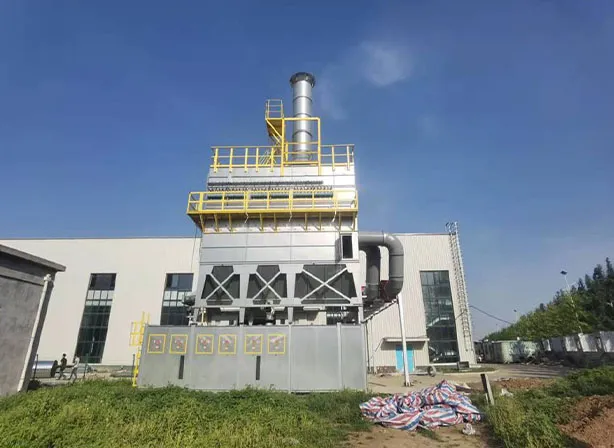
What the safeguards look like in practice on a woodworking installation: explosion relief on both the mainframe and the silo, isolation between the collector and the occupied building, temperature monitoring on the storage volume, spark detection where the upstream process can generate ignition sources, and fire suppression at the silo. Company-level compliance statements cover ISO 9001:2015 quality management and CE compliance; note the September 2026 ISO revision when checking documentation validity.
Buying on airflow alone. A unit rated for your calculated flow but not for your system’s static pressure at dirty-filter condition will not deliver that flow. Both figures belong in the comparison.
Sizing for the current machine list. Furniture plants add machines. Zero headroom means a second collector within a few years, and the second collector costs more than the headroom would have.
Treating the silo as the last decision. It has the longest civil-works lead time of anything in the package and the hardest physical constraint (discharge height versus collection vehicle).
Assuming compact units scale up. Two or three shop-tier collectors ducted together do not become a plant system. They multiply maintenance points, each returns filtered air into the workshop volume, and none of them solves centralized storage.
Skipping the dust hazard analysis to save four weeks. The findings change the equipment list. Running the analysis after the order is placed means either a variation or an unprotected system.
Compared with the individual bag-type and cyclone collectors common in smaller woodworking shops, a centralized system removes dust from the building rather than filtering and returning it, gives one maintenance schedule instead of twenty, publishes an emission target, and integrates storage. Those are real advantages and they are why factory-tier plants buy them.
What it costs:
For a plant of eight machines in a leased building with an uncertain lease, distributed units genuinely may be the better answer. For a plant that owns its site and is adding capacity, the arithmetic usually runs the other way within the first replacement cycle of the distributed filters.
A: Calculate it rather than estimating: total the airflow required at every machine port, apply a justified simultaneity factor, and match the result against rated airflow and static pressure. Most production plants land somewhere inside the 30,000–150,000 m³/h band covered by CP and CC Series.
A: Yes, with a trade-off. Either split into two filtration sections sharing one silo, or specify a single mainframe for the finer duty and accept shorter media life. The catalogue splits CP (fine/ultrafine) and CC (medium/large particle) precisely because the two loads behave differently.
A: Roughly 15 kW equates to the top of the compact tier, around 15,000 m³/h. That covers a small workshop or one fine-dust cell. It does not cover a ducted network across a production floor, and it does not address bulk storage.
A: Kilograms of waste per hour × hours between collections ÷ bulk density of your actual waste mix. MS Series covers 25–94 m³ with a discharge height of approximately 3,100 mm; DC Series tower silos cover 30–100 m³ in a smaller footprint at 10,000–18,000 mm tall.
A: The published wording is that explosion protection is designed based on ATEX principles. Product certificate numbers and issuing bodies are not publicly disclosed. Where a project requires certified equipment, request the specific certificate.
A: Available on request based on system configuration and project requirements. The configuration variables — airflow, dust type, layout, ducting, filtration, safety level — move the number too much for a published price to be meaningful.
A: Lead time depends on configuration and is confirmed per project. The item to watch in the programme is not the equipment: it is the foundation and, for tower silos, the crane lift.
Before you request quotations: measure the clear height under the lowest obstruction in your building, and measure the bed height of whatever vehicle will collect the waste. Those two numbers eliminate more unsuitable configurations in five minutes than a week of specification comparison will. If your plant also runs a finishing or coating line, solvent VOC treatment is a separate design track with its own capture and adsorption questions, and it should be scoped alongside the dust system rather than after it.
Senserui is an industrial environmental equipment manufacturer specializing in dust collection and VOC treatment systems. His work focuses on engineering-driven system design, modular standardization, manufacturing consistency, and the development of safer and more maintainable industrial air-pollution-control solutions. Senserui was founded in 2017 and manufactures from an approximately 10,000 m² production base in Qingdao, China, with in-house airflow, noise and filter testing before delivery. Technical review by the Senserui Engineering Team, covering system engineering, process planning, quality control, assembly and commissioning, after-sales support and IoT-based system operations.