For a faster response, please include your WhatsApp or Skype in your message so we can contact you as soon as possible.
To help us respond faster, please leave your WhatsApp, email, or project details. We usually reply within 24 hours. For urgent inquiries,contact us on WhatsApp: +8617862411260 or WeChat: +8617862411260. call us directly.
A dust explosion in a silo occurs when combustible wood or process dust, suspended in air inside a confined storage vessel, ignites and the resulting pressure has no safe path to escape except through explosion relief panels, connected ductwork, or the silo structure itself.
Combustible dust needs five things to ignite: fuel, oxygen, an ignition source, dispersion into a cloud, and confinement. A woodworking floor has the first four almost constantly — sawdust, ambient air, a spark source somewhere in the process, and enough disturbance to keep particles airborne. What a silo adds is the fifth element. Confinement turns a flash fire that would otherwise dissipate in open air into a pressure event, because the expanding gas has walls to push against instead of open space to bleed into.
This is why silo-specific incidents read differently from shop-floor fires in industry reports. The ignition event itself is often small — a smoldering ember carried in from an upstream process, a static discharge during filling — but the confined geometry amplifies the consequence rather than the cause.
Two operating states raise silo risk above baseline, and neither is the quiet steady-state period when the silo just sits full.
During filling, dust is actively dispersed into a cloud as material drops from the inlet duct. This is the moment dust concentration inside the vessel is most likely to sit within an explosible range — too little dust in the air won’t sustain a flame front, but the fine particulate stream coming off a centralized collection system during active filling routinely does.
During discharge, the opposite problem shows up: as material empties out, air is pulled in to replace it, and any smoldering material trapped near the outlet gets a fresh oxygen supply at exactly the wrong moment. Bridging or rat-holing in the stored material can also create sudden collapses that disperse settled dust back into suspension.
The interconnection between the silo and the upstream dust collector deserves separate attention here. A silo is rarely an isolated vessel — it’s fed by ductwork from a centralized mainframe, and that ductwork is a propagation path in both directions. Flame or pressure generated inside the silo can travel back up the duct toward the collector and the rest of the system; conversely, an ignition source originating at the collector can travel down into the silo. This is the reasoning behind isolation devices between the two vessels in a properly designed system, separate from whatever protection each vessel carries on its own.
Explosion relief venting is designed to open at a set pressure threshold and let the expanding gas and flame front escape outward through a controlled panel, rather than through the weakest point of the silo shell, which is usually a weld seam or an access door not built to fail predictably. That’s the entire function: relief venting manages where the pressure goes, not whether ignition happens in the first place.
This distinction matters because explosion relief is sometimes discussed as if it prevents the event. It doesn’t. A properly sized vent reduces the peak pressure the structure experiences and directs the discharge to a safe location — outdoors, away from personnel and adjacent equipment — but the ignition still occurs, the flame front still develops, and anything inside the discharge path at the moment of venting is still exposed. Vent sizing depends on the vessel’s volume, the dust’s specific explosibility characteristics (Kst value), and the reduced pressure the structure can tolerate — figures that come from dust hazard analysis specific to the material being stored, not from a generic table.
Where relief venting manages an explosion in progress, temperature and water-pressure monitoring are aimed earlier in the sequence — at catching a smoldering condition before it becomes an open flame or a full deflagration.
Temperature monitoring inside a storage silo tracks for the gradual heat buildup associated with a smoldering nest, which behaves very differently from an open flame and can go undetected by simple visual inspection for hours. Water-pressure monitoring, paired with fire suppression, confirms that the suppression system connected to the silo actually has the pressure available to discharge when triggered — a detail that matters because a suppression system with an undetected pressure fault is a system that looks compliant on paper and does nothing in an actual event.
Neither of these replaces explosion relief, and explosion relief doesn’t replace either of them. They address different points in the same failure sequence: monitoring catches conditions before ignition where possible, and relief venting manages the outcome if ignition happens anyway.
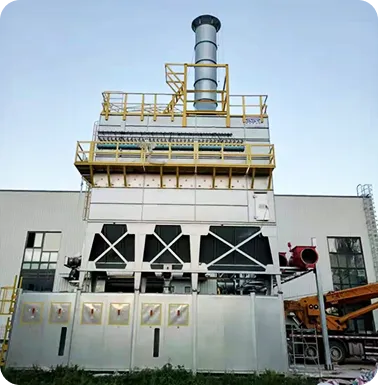
Senserui’s two storage silo lines are built around different structural approaches, and the two also differ in what safety features are publicly documented for each — a distinction worth reading carefully rather than assuming parity between the two.
| Parameter | MS Series Integrated Dust Bin | DC Series Intelligent Modular Tower Silo |
| Structure type | Rectangular integrated dust bin, paired with centralized collection systems | Modular tower-type silo |
| Storage capacity | 25–94 m³ | 30–100 m³ |
| Rated power | Not applicable (passive storage) | 5–15 kW |
| Footprint | ~3,500–13,000 mm length × ~2,400 mm width | ~2,400–4,500 mm diameter |
| Height | Discharge height ~3,100 mm | ~10,000–18,000 mm |
| Published safety features | Explosion relief, fire suppression, temperature monitoring, water-pressure monitoring | Designed with reference to relevant national and EU standards; specific safety-feature list and product certificate number not published on the reviewed page |
That gap in the DC row isn’t a flaw in the product — it’s a gap in what’s currently published, and it’s worth being direct about rather than assuming the two systems carry identical protection. A buyer evaluating a DC tower silo for a combustible-dust application should confirm the specific safety feature set for that model directly rather than assuming it matches the MS line’s documented configuration.
A frequent assumption is that a silo marketed toward woodworking applications comes pre-configured with explosion protection sized for that facility’s specific dust. It doesn’t work that way. Vent sizing and suppression system design depend on the volume of the specific vessel, the Kst value of the specific dust being stored — which varies by wood species, moisture content and particle size — and the layout of the specific installation. A silo model rated for a general woodworking application is a starting configuration, not a finished safety calculation for your plant.
A: No. Venting manages the pressure and flame path after ignition occurs, directing it to a controlled discharge point. It doesn’t stop the ignition event itself — that depends on controlling ignition sources and dust concentration in the first place.
A: Not without a hazard analysis specific to that facility’s dust. Kst values and required vent sizing vary by wood species, moisture content and particle size, so a general product rating is a starting point, not a completed calculation.
A: The ductwork linking them is a propagation path in both directions — flame or pressure generated in one vessel can travel toward the other unless isolation devices are in place. Treating the silo and collector as independently protected without addressing that connection leaves a gap.
A: No, they address different stages of the same risk. Temperature monitoring is aimed at catching a smoldering condition before it develops into an open flame; explosion relief manages the outcome if ignition happens regardless. A system needs both layers, not one in place of the other.
This overview is intended as general technical background on silo explosion protection principles, not as a substitute for a facility-specific dust hazard analysis. If you’re evaluating protection requirements for an active combustible-dust process, that assessment should be performed against your specific material and installation, not inferred from a product’s general feature list.